DLG multi-spindle drilling machine
The high-speed drilling machines with mechanical guides.
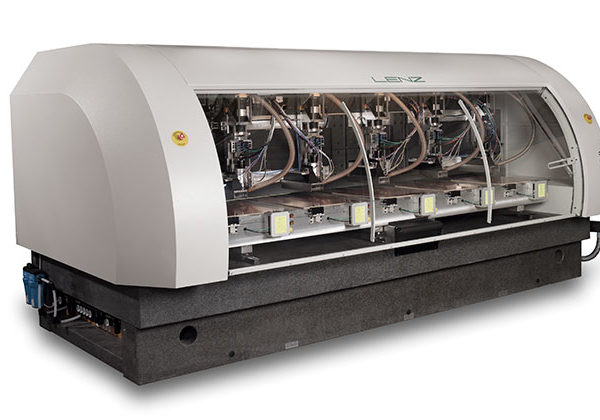
High-speed drilling machines with mechanical guides
The increased number of holes per PCB, and the longer drilling time that comes with it, can be countered optimally by more powerful linear motors.
To make full use of the more powerful and thus even more dynamic linear drives, LENZ uses mechanical linear guides developed specifically for linear drives. With this machine concept, even 6-spindle machines can reach a drilling frequency that was previously not even conceivable with 1-spindle machines.
| Guides | Linear guides with ball chain |
| Drives | Linear motors in X, Y and Z axes |
| Clamping system | Variable for locating pins from 3 to 5 mm |
| Tool magazine | EUROMAGAZIN |
| CNC | CNC 84.00, PC-based |
Technology of the multi-spindle drilling machines
Latest linear guide technology
What has been standard for ball bearings for over a hundred years is now also used for linear guides. Normal linear guides are full-ball.
The new linear guides used by LENZ have a ball chain, just like ball bearings. The ball chain prevents metallic point contact between the balls. The elimination of the opposing rotation of the balls leads to very smooth running and very little wear.
Maximum dynamics – linear motor in the Z axis
Virtually wear-free drives in the X and Y axes have long been standard at LENZ; these drives, with all their advantages, are now also available for the Z axis. Maximum dynamics with almost no wear — ideally suited for micro and depth drilling.
The connection of the pressure foot was also developed for precise depth drilling and milling. Like the spindle holder, the pressure foot is guided by linear guides, which ensures the “stiff” connection required for depth drilling and milling.
The variable clamping system
… is designed for locating pins from 3 to 5 mm, which are monitored for exact positioning in the prism. The contact surfaces are made of wear-free carbide.
Micro-drilling with swivelling pressure foot
A pressure foot with the smallest opening almost completely surrounds the drill and thus enables exact micro-drilling.
During tool changes, the pressure foot swivels from the working position (1) to the tool change position (2), releasing the drill.
Continuously active drill breakage detection
The tool is monitored continuously while drilling. If the drill breakage detection system detects a broken tool, drilling is stopped immediately, logged and continued independently.
Tool measurement with laser beam
With the LENZ laser measuring system, the tool is checked for exact diameter, concentricity and clamping length at every tool change. Specified tolerance ranges are taken into account. If a tool is outside these ranges, it is automatically replaced by another. Together with the laser measuring system, drill breakage detection is the prerequisite for trouble-free and safe fully automatic operation in the so-called “ghost shift”.
Several hundred tools
LENZ as a pioneer. What LENZ developed in 1985 is now the worldwide standard as the EUROMAGAZIN. The tools are prepared in the EUROMAGAZIN and inserted completely into the exchangeable tool plates.
Machine control
On single- and two-spindle machines, the Sieb & Meyer control and the machine electrics are integrated in the base to save space and can be pulled out to the front for service work. On request, the information monitor and keyboard can be mounted on a swivel arm on the machine. From three-spindle machines onwards, the CNC and the machine electrics are housed at the rear of the machine.
The proven PC-based CNC 84.00 control is available for all series.